Discover a fertilizer pellet cooler in Chile for cooling 3–5 mm organic fertilizer granules. Explore the SKLF17*17 counterflow cooler, 6–8 T/H capacity, technical features, and production line integration.
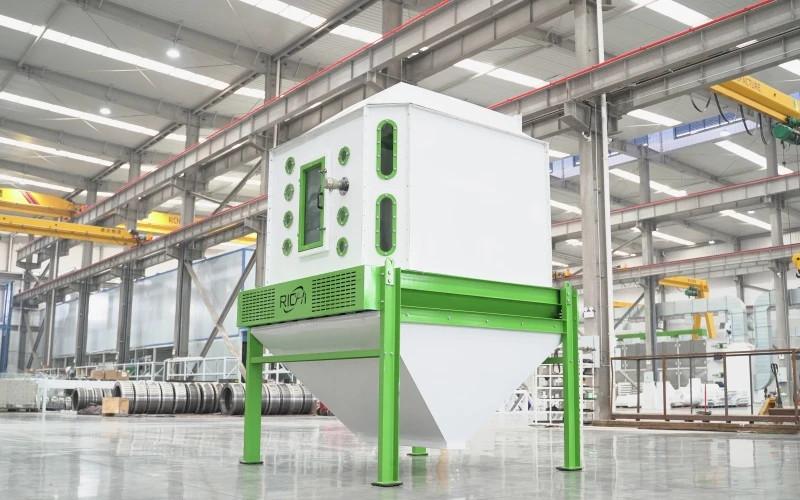
A fertilizer pellet cooler in Chile was selected by a medium-sized organic fertilizer manufacturer looking to improve the handling of finished granules without replacing its existing production equipment. The plant processed composted poultry manure, livestock manure-based organic matter, and selected agricultural residues into granular fertilizer for agricultural customers.
Although its granulation section was capable of meeting normal production requirements, hot granules leaving the forming stage created difficulties during screening, conveying, and temporary storage. The manufacturer therefore purchased one RICHI SKLF17*17 counterflow cooler as an independent equipment upgrade.
Name:
Fertilizer Pellet Cooler
Country:
Chile
Date:
2026
Capacity:
6–8 T/H
Model:
SKLF17*17
Power:
1.5 kW
cooling time:
6–15 minutes
finished granule size:
3–5 mm
The project focused on approximately 3–5 mm organic fertilizer granules intended for soil improvement and nutrient management in horticultural production, orchards, and other agricultural applications. The customer wanted a more controlled cooling process, less accumulation of warm material before screening, and more consistent finished-product handling.
Rather than investing in a complete organic fertilizer pellet production line, the plant retained its existing mixing, granulation, and packaging equipment and added a dedicated cooler after the fertilizer granulator machine. This approach addressed a specific production bottleneck while keeping the scope of the investment manageable.
Chile has a varied agricultural sector, including fruit production, vineyards, vegetable cultivation, and intensive horticulture. These industries use different soil management and fertilization practices, creating opportunities for commercial fertilizers and soil-conditioning products. Organic fertilizer manufacturers can serve farms and distributors that require granulated products suitable for bulk handling, transport, and controlled application.
The customer in this project operated a regional fertilizer processing facility supplying agricultural customers rather than a large integrated chemical fertilizer complex. Its raw materials included composted poultry manure, livestock manure-derived organic matter, and plant residues collected from agricultural activities. The exact formulation varied according to feedstock availability, compost maturity, nutrient targets, and the characteristics required in the finished product.
Before the upgrade, freshly formed granules moved from the granulation stage into downstream handling while still carrying substantial process heat. Depending on moisture content and formulation, these granules could be relatively warm and mechanically vulnerable. Material accumulated when the screening and conveying stages could not accept it at the same rate as the granulator discharged it. Operators consequently had to pay closer attention to material flow and avoid allowing the post-granulation section to become congested.
Cooling is important because finished fertilizer granules must be prepared for subsequent screening, conveying, storage, and packaging. Granules that are packed before they have cooled sufficiently may retain excess heat, and moisture migration or condensation under unsuitable storage conditions can contribute to caking. These risks depend on the material formulation, moisture level, packaging, and storage environment; a cooler is one part of controlling them rather than a substitute for proper moisture management.
The manufacturer decided that an additional cooling machine was a more practical solution than replacing the granulator or rebuilding the entire plant. The new unit would be installed after the existing granulation section, allowing hot granules to pass through a dedicated cooling stage before continuing to screening and finished-product handling.
RICHI recommended the SKLF17*17 model for this medium-scale application. Its listed rated throughput is 6–8 T/H, with a drive power of 1.5 kW. This capacity range provides a reference for matching the cooler to the expected production rate of the existing granulator, although the final working capacity must be confirmed using the actual fertilizer formulation and operating conditions.
| Project specification | Details |
|---|---|
| Core keyword | Fertilizer pellet cooler in Chile |
| Equipment | Counterflow fertilizer pellet cooler |
| Selected model | SKLF17*17 |
| Rated throughput | 6–8 T/H |
| Listed drive power | 1.5 kW |
| Typical cooling time | 6–15 minutes |
| Reference discharge temperature | Approximately 3–5°C above ambient temperature |
| Representative finished granule size | 3–5 mm |
| Material handled | Granulated organic fertilizer made from composted manure-based material and selected plant residues |
| Purchase scope | One standalone cooling machine |
| Shipping origin | Qingdao Port, China |
| Destination port | Port of San Antonio, Chile |
The SKLF17*17 uses a counterflow cooling arrangement in which cooling air moves against the direction of material travel. This arrangement supports progressive heat removal as granules pass through the cooler. The reference cooling time is approximately 6–15 minutes, and the listed discharge temperature is around 3–5°C above ambient temperature under suitable operating conditions.
These figures are equipment reference specifications rather than guaranteed results for every fertilizer formulation. Organic fertilizer granules can differ considerably in density, porosity, moisture content, surface condition, and mechanical strength. The actual cooling performance depends on these properties, the inlet temperature, airflow, material-bed depth, ambient conditions, and operating rate. The final configuration should therefore be checked against the customer's production data before installation.
The plant's principal product is granulated organic fertilizer made from composted manure-based material and selected agricultural residues. Poultry manure can contribute organic matter and plant nutrients, while suitable plant residues help form part of the composting feedstock. Livestock manure-derived materials may also be used when their quality and availability suit the formulation.
These materials require appropriate preparation before granulation. Composting and maturation help stabilize organic feedstocks, while screening and size reduction may be necessary to achieve a more uniform mixture. The formulation must also be managed for moisture, particle distribution, and binding characteristics so that the granulator can produce granules with suitable strength and size.
For this project, 3–5 mm granules were selected as the representative finished-product specification. Granules in this range can be suitable for bagged organic fertilizer and soil-conditioning products, subject to the customer's product design and the requirements of the intended application. The granulator determines the initial granule formation, while the cooling machine reduces product temperature before the granules proceed to screening and packaging.
Once discharged from the granulator, the hot fertilizer granules enter the cooler and pass through a controlled cooling process. The cooled material then moves to the screening section, where fines and out-of-specification particles can be separated. Accepted granules are conveyed to storage or packaging, depending on the plant's product handling arrangement.
The cooling stage does not replace drying or compost maturation. If the incoming material contains excessive moisture or has not reached the required degree of stability, cooling alone will not correct those problems. The plant must control the upstream preparation process and use cooling to manage the temperature of properly formed granules.
One of the main requirements in fertilizer granule cooling is uniform material distribution. If granules form an uneven bed inside the cooling chamber, airflow can pass more easily through thinner sections while thicker areas receive less effective cooling. The result may be variation in discharge temperature even when the average production rate appears satisfactory.
The SKLF series uses a four-way adjustable distributor to spread incoming material across the cooling chamber. This helps the plant establish a more even material bed and make better use of the available cooling area. Mechanical material-level control supports stable operation by helping maintain the required level of material in the chamber.
The SKLF Counterflow Pellet Cooler also uses a swing-flap discharge mechanism controlled by a flexible hydraulic transmission system. The discharge arrangement is designed to release cooled material smoothly, reducing unnecessary impact that could damage mechanically weak granules. This is particularly relevant when finished-product appearance and the proportion of intact granules matter to the customer.
The octagonal cooling chamber is designed to reduce dead zones where material might otherwise remain trapped. A curved discharge hopper supports material flow and helps limit residue accumulation. Stainless steel is used for the upper section of the cooler and the rotary airlock feeder to improve corrosion resistance in areas exposed to material and normal operating conditions.
For larger cooling applications, an optional powered rotary leveling mechanism can help maintain a more uniform material layer. Although this feature is not necessarily required for every medium-capacity installation, it can be considered when the material has uneven flow characteristics or when the project requires closer control of the bed distribution.
The customer's existing plant already had equipment for raw-material preparation, mixing, granulation, and packaging. The main limitation was the handling of hot granules after the granulator. Replacing the entire line would have involved a broader capital investment, additional installation work, and more disruption to normal production.
Adding one fertilizer pellet cooler offered a more focused alternative. The upgrade was intended to create a dedicated cooling stage between granulation and screening, improving the flow of material through the downstream section without changing every machine in the plant.
This type of project requires more than choosing a cooler based on its rated throughput. The incoming granulator must supply material at a suitable rate, while the screening equipment, conveyors, and packaging section must be able to handle the cooled output. If one of these stages has insufficient capacity, increasing cooling capacity alone will not remove the overall production bottleneck.
The SKLF17*17's listed drive power is 1.5 kW, but this figure should not be interpreted as the total electricity demand of the complete cooling arrangement. Depending on the installation, the cooling system may also require a fan and other auxiliary equipment. The electrical plan should account for all supplied and connected components.
Organic fertilizer granules behave differently from conventional animal feed pellets. Their moisture content, density, porosity, surface condition, and mechanical strength depend on the composted materials, formulation, binder, and granulation process. These factors influence the way the material moves through the cooler and how effectively heat is removed.
For this Chilean project, the installation review should establish the actual granulator output, typical granule diameter, inlet temperature, material moisture, available installation height, and downstream conveyor capacity. The cooler's inlet and outlet connections must also match the plant layout, allowing material to pass through without unnecessary transfer points or excessive drops.
RICHI can provide equipment dimensions, layout information, interface guidance, and model-selection support to help coordinate the new machine with the existing line. Reviewing these details before shipment reduces the risk of avoidable installation changes and helps the customer prepare the required foundations, electrical connections, access space, and maintenance clearances.
During commissioning, operators should observe the distribution of granules inside the chamber, check the material-level control, and verify the discharge mechanism. Inlet and outlet temperatures should be recorded at a stable operating rate. If the granules are not cooling evenly, the first checks should include material distribution, airflow, feed rate, bed depth, and incoming moisture rather than simply increasing the production rate.
Routine maintenance should include inspection of the drive components, discharge mechanism, seals, air passages, and areas where fertilizer dust or residue may accumulate. Regular cleaning and inspection are particularly important when the plant processes different formulations, since residual material can contaminate subsequent batches or affect the flow of the next product.
The equipment is planned for sea shipment from Qingdao Port in China to the Port of San Antonio in Chile. San Antonio is a major Chilean commercial port and a practical destination for imported industrial machinery serving the country's agricultural and manufacturing sectors.
Before dispatch, the equipment should be checked against the agreed order specifications, including the model designation, drive rating, supplied components, protective packaging, and shipping documents. Clear identification of the main machine and accessories makes arrival inspection and installation preparation more straightforward.
The importer should confirm the applicable machinery import requirements and shipping documentation for the specific consignment before dispatch. These requirements should be checked against the current rules and the details of the actual shipment rather than assumed to be identical for every import order.
After the cooler was integrated into the existing production arrangement, the plant's operating team placed particular emphasis on the transition between granulation, cooling, and screening. The practical value of the upgrade was not simply the presence of another machine; it was the opportunity to control the temperature and movement of granules before they reached the next process stage.
The production manager's assessment focused on three points: whether the cooler could accept the granulator's normal discharge, whether the cooled material could move steadily into screening, and whether operators could adjust the process without repeatedly interrupting production. The team also monitored the condition of granules after discharge, since excessive breakage would increase the amount of material requiring reprocessing.
For the plant, the most useful acceptance criteria were measurable operating indicators rather than a general claim of improved performance. These included stable material flow, consistent outlet temperature under comparable operating conditions, manageable fines generation, and reliable coordination with the existing screening and conveying equipment.
These operating checks provide a practical basis for evaluating the investment over time. If the plant later expands its output or introduces a different fertilizer formulation, the same records can help determine whether changes to airflow, feed rate, material distribution, or downstream handling are required.
The fertilizer pellet cooler in Chile project demonstrates how a single cooling machine can address a specific process requirement in an existing organic fertilizer plant. By selecting the SKLF17*17 counterflow cooler, the manufacturer added a dedicated cooling stage for approximately 3–5 mm organic fertilizer granules without committing to a complete production line replacement.
The selected model has a listed throughput of 6–8 T/H, a drive power of 1.5 kW, and a typical cooling time of 6–15 minutes. Its counterflow arrangement, adjustable distributor, material-level control, swing-flap discharge mechanism, and chamber design are intended to support progressive cooling and controlled discharge. Actual results depend on the properties of the granules and the conditions under which the equipment operates.
For fertilizer manufacturers evaluating a pellet cooling machine, the most useful starting point is the actual material and production requirement. Granule size, inlet temperature, moisture content, bulk density, mechanical strength, and target throughput all affect equipment selection. The cooler must also fit the capacity of the granulator, screening system, conveyors, and packaging equipment.
RICHI Machinery can assist with model selection, equipment layout, technical coordination, and installation planning for fertilizer pellet cooling applications. Manufacturers considering a new installation or a targeted upgrade can provide their expected throughput, granule specifications, material moisture, inlet temperature, and existing process layout to identify a suitable cooling configuration.
Having the right mix of reliable, high-quality pellet machine and pelletizing systems and expert support is essential to your success. Watch how our end-to-end feed pellet plant solutions have helped our customers optimize their performance.
Our customized and future-proofed turnkey pellet plant solutions is designed with you at the core. From vision to reality and beyond, our team stays connected with yours. Giving you peace-of-mind with an expert at your side.
At RICHI, we go beyond project completion. With RICHI Servicee, we’re your dedicated partners in success. Count on us for expert guidance, minimal downtime, and optimized productivity. Choose RICHI for unmatched service and support.

Meet global product demands and quality standards with industry-leading pellet plant design, engineering, equipment, and construction services for pellet processors.

Your Partner Beyond Project Completion
2000+ cases
RICHI is the leading designer, manufacturer and builder of pellet plants in the world, completing over 2000 projects in 140 countries across 6 continents.
Read More
Increase plant productivity, profitability, and safety by integrating high quality equipment into your pellet production line. Over the years, RICHI has become China's top pellet equipment manufacturer. At the same time, RICHI has established valuable partnerships with the world's leading component and raw material manufacturers to bring you the best there is in technology, automation, and efficiency in pelleting plant machinery.

For nearly 30 years, RICHI has been providing best-in-class pellet plant equipment and services to clients across a variety of industries, sizes, and needs. We pride ourselves on the knowledge and skill that each team member possesses – from our technical sales team to our process design engineers. You can count on RICHI Machinery to take your operation to the next level of innovation, quality, and success.
Need help with your pellet manufacturing plant project? Contact us today.
ANIMAL FEED
BIOMASS
WOOD
ORGANIC FERTILIZER
AQUA FEED
CAT LITTER
MUNICIPAL WASTE RECYCLING
SPECIAL PELLET PRODUCTION
RICHI Machinery continues to deliver world class pellet mill equipment, pellet plant engineering and project solutions that add value to our customers in the animal feed, wood waste, agriculture waste, organic fertilizer, cat litter and special pellet products industries. Throughout the years, we RICHI Machinery have built strong brand, becoming industry-leading pellet machine manufacturer. We value integrity, promise quality, and prioritize your success.
Learn MoreWith our expert team, we precisely implement your process engineering requirements in pellet mill and pelletizing plant systems. No matter which industry you’re in – we understand your needs and deliver solutions that meet the highest standards.
At RICHI, quality comes first. Our pellet making machine and related pellet line equipment undergo rigorous quality controls to ensure they meet the highest standards. Rely on products that are durable, safe, and efficient.
With decades of experience in pellet machine and pellet production line production, we have earned a reputation as a trusted partner in various industries. Our expertise allows us to cover a wide range of applications.
Not only do we offer premium pelleting equipment, but we are also experts at designing, building, installing, and maintaining facilities from the ground up. Our expertise is within pellt plant process design, discovering the most efficient, productive, and profitable way to handle your materials in an end-to-end cycle.
○ RICHI MACHINERY
Keeping in touch with us is an effective way to solve all your problems. If you have any needs or questions, please leave your contact information, then RICHI technical consultants will send design, quotation, videos to your mailbox. You can also contact us directly via WhatsApp: +86 13838389622
Copyright©2015-2026 by HENAN RICHI MACHINERY CO., LTD. All rights reserved.