RICHI supplied a 3–4 T/H Beet Pulp Drying System in Kenya to dry pressed sugar beet pulp from 76–78% moisture to 10–12%, evaporating 2.2–3.0 T/H water.
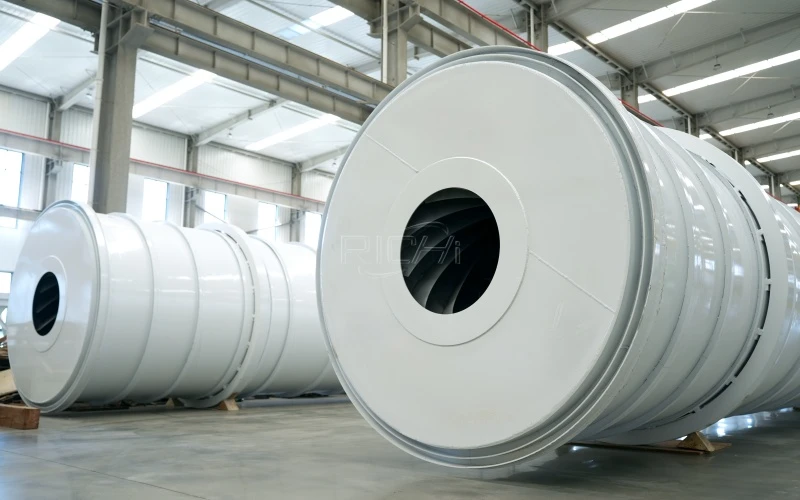
A dairy-feed manufacturer in Kenya's Rift Valley selected one RICHI Beet Pulp Drying System in Kenya to develop a local drying route for pressed sugar beet pulp. The company operates its main feed business near Nakuru but located the drying section closer to an emerging sugar-beet processing source in Nyandarua County. This arrangement avoids transporting unnecessary water over a longer distance before drying and gives the customer access to a fibrous feed ingredient that can later be incorporated into dairy cattle formulations.
The selected φ1.8×12×3C three-pass rotary drying system uses a 30 kW drum drive. The project is designed around approximately 3–4 T/H of pressed beet pulp at roughly 76–78% moisture. At a finished moisture target of approximately 10–12%, the dryer removes around 2.2–3.0 T/H of water and produces approximately 0.8–1.0 T/H of dried beet pulp. These three figures — wet feed, evaporation load and dry-product output — are treated separately throughout the project.
Name:
Beet Pulp Drying Machine
Country:
Kenya
Date:
2026
Capacity:
3–4 T/H
Model:
φ1.8×12×3C
Drum Drive Power:
30 kW
Incoming Moisture:
76–78%
Main Product:
Dried beet pulp for dairy cattle feed
Kenya's commercial sugar-beet sector is still small compared with its established sugarcane industry. This project therefore does not assume that large quantities of wet beet pulp are already available throughout Nakuru and the wider Rift Valley. Instead, the feed manufacturer works with an emerging beet-processing source in the cooler Nyandarua highlands, where commercial sugar-beet cultivation and processing have begun to develop.
Pressed beet pulp contains mostly water. Moving several tonnes of wet material to Nakuru before drying would mean paying to transport water. The customer therefore established the thermal drying section near the pulp source and moves the much lighter dried product to its existing feed operation after cooling and storage stabilization.
This arrangement also reduces the time that highly moist pulp remains in uncontrolled storage before preservation.
| Project Parameter | Specification |
|---|---|
| Equipment | Three-pass rotary beet pulp drying system |
| Model | φ1.8×12×3C |
| Drum Diameter | Approximately 1.8 m |
| Effective Drum Length | Approximately 12 m |
| Drum Drive Power | 30 kW |
| Wet Feed Capacity | Approximately 3–4 T/H |
| Incoming Moisture | Approximately 76–78% |
| Water Evaporation Capacity | Approximately 2.2–3.0 T/H |
| Dry Product Output | Approximately 0.8–1.0 T/H |
| Final Moisture | Approximately 10–12% |
| Main Product | Dried beet pulp for dairy cattle feed |
The 30 kW figure is the mechanical power required to rotate the dryer drum. It is not the thermal power required to evaporate water. Furnace duty, fuel consumption and process-air volume are calculated separately from the actual evaporation load and heat-source efficiency.
Dryer selection starts with dry matter rather than drum dimensions alone. If 4 T/H of pressed beet pulp enters the system at 78% moisture, the material contains only about 0.88 T/H of dry solids. At approximately 11% final moisture, those solids correspond to just under 1 T/H of dried product.
The difference — approximately 3 T/H — is the water that must be evaporated. This is why the project's upper operating point is expressed as approximately 4 T/H wet feed, 3 T/H evaporation and 1 T/H finished product rather than describing all three figures as the same dryer capacity.
If incoming pulp moisture falls closer to 76%, dry-product output increases slightly and the evaporation requirement falls. If wetter pulp arrives, the operator either reduces wet-feed rate or improves upstream mechanical dewatering.
Thermal evaporation is one of the most energy-intensive stages in beet pulp processing. The customer therefore requires the beet-processing partner to supply pressed pulp rather than very dilute pulp directly from extraction.
Mechanical dewatering removes free water without paying the thermal cost of evaporating it. The drying system then handles the remaining bound and retained moisture required to reach approximately 10–12% final moisture.
Incoming moisture is checked routinely. The dryer is not operated at the same 3–4 T/H feed rate regardless of whether the pulp arrives at 72%, 78% or 81% moisture. Each change alters the evaporation load substantially.
The customer had limited space available at the satellite drying site, making a compact drum arrangement attractive. The three-pass structure provides a longer material and hot-air path inside a relatively compact installation footprint.
That does not mean a three-pass dryer is universally superior to a single-pass unit for every beet pulp project. Selection depends on pulp consistency, tendency to form lumps, evaporation demand, available floor area and heat-source design.
For this system, a controlled receiving hopper and metering/dispersing screw prepare the pressed pulp before it enters the drum. This reduces large wet clumps and gives the dryer a more consistent feed, which is especially important for fibrous press cake.
The system does not use one permanent 380–450°C inlet-gas setting simply because that range appeared in an initial equipment specification. Gas temperature must be managed together with feed rate, airflow, incoming moisture and exhaust condition.
The control objective is final product moisture and stable feed quality rather than maintaining one temperature number. Operators monitor inlet conditions, exhaust temperature, outlet moisture and product appearance and then adjust fuel input or wet-feed rate accordingly.
The same principle applies to residence time. Drum speed affects material movement, but residence time cannot be specified independently of loading and airflow.
The customer selected a biomass hot-air furnace because pipeline natural gas is not available at the project site and relying exclusively on diesel would expose the dryer to higher fuel-price volatility. The furnace can use suitable dry agricultural or wood-processing residues that meet the combustion-system specification.
Fuel quality is checked for moisture, ash and particle size before use. Low-density agricultural residues require controlled feeding and combustion-air distribution, while high-moisture fuel can sharply reduce useful heat output.
The project does not claim one fixed biomass consumption per tonne of dried pulp. Actual fuel use depends on evaporation load, fuel calorific value, moisture, furnace efficiency and heat losses.
Pressed beet pulp cannot be stored for long periods in the same way as a dry feed ingredient because its high water content creates rapid deterioration risk. Drying to approximately 10–12% moisture changes the handling and storage condition substantially.
The rotary dryer is not operated simply to reach the lowest moisture possible. Overdrying wastes thermal energy and can reduce saleable product mass. The customer instead targets a storage-stable specification suitable for subsequent feed handling.
Moisture verification is performed on the finished material rather than assuming that a particular exhaust temperature automatically means the product has reached 12%.
Dried beet pulp leaves the thermal section warm and must be cooled before it is placed into enclosed storage or transported to the main feed mill. Packing or binning hot material can encourage condensation and moisture migration as the product cools.
The existing downstream cooling and conveying section therefore handles approximately 0.8–1.0 T/H of dry product rather than the 3–4 T/H wet-feed rate entering the dryer.
After cooling, the dried pulp can be transported to Nakuru and incorporated into dairy cattle feed formulations or supplied as a separate feed ingredient according to the customer's sales plan.
The customer's actual application is dairy cattle feed. Beet pulp provides highly fermentable fiber and can form part of a dairy ration, but it is not a complete feed and the dryer does not determine its inclusion rate.
The feed mill combines dried beet pulp with forage, cereals, protein ingredients, minerals and other components according to the nutrition program. Its role can therefore differ between farms depending on available forage and the rest of the ration.
The project does not claim a fixed increase in milk yield from using dried beet pulp. Feeding response depends on the complete diet, cow production level, dry-matter intake and farm management.
Unlike countries with long-established beet sugar industries, Kenya cannot yet assume year-round large-volume beet pulp availability. The customer therefore sizes this project around confirmed supplier tonnage rather than national sugar-beet production projections.
Raw-material agreements cover campaign volume, expected pressed-pulp moisture and delivery schedule. If commercial beet acreage expands, the plant can evaluate longer operating hours or additional drying capacity from actual wet-pulp availability.
This makes feedstock security just as important as dryer capacity in the investment decision.
The Beet Pulp Drying System in Kenya is prepared for export from Qingdao, China, in modular sections and enters the country through the Port of Mombasa before inland delivery to the Nyandarua-area drying site.
Before shipment, RICHI reviews the wet-pulp receiving hopper, metering screw, drum foundation, hot-air furnace, fan and duct system, exhaust dust control, dry-product cooler, electrical supply and site layout. Thermal-load calculations are handled separately from the 30 kW mechanical drum drive.
This Beet Pulp Drying System in Kenya project uses one φ1.8×12×3C three-pass rotary dryer with a 30 kW drum drive at a satellite processing site serving a Rift Valley dairy-feed manufacturer. Pressed sugar beet pulp enters at approximately 76–78% moisture and around 3–4 T/H. The system removes approximately 2.2–3.0 T/H of water and produces roughly 0.8–1.0 T/H of dried pulp at approximately 10–12% final moisture.
For another project, RICHI Machinery needs confirmed wet-pulp supply, inlet moisture, dry-matter analysis, final moisture target, heat source, operating schedule and downstream cooling and storage information. These figures determine whether a three-pass dryer of this scale is technically justified far more reliably than selecting equipment from wet tonnage alone.
Having the right mix of reliable, high-quality pellet machine and pelletizing systems and expert support is essential to your success. Watch how our end-to-end feed pellet plant solutions have helped our customers optimize their performance.
Our customized and future-proofed turnkey pellet plant solutions is designed with you at the core. From vision to reality and beyond, our team stays connected with yours. Giving you peace-of-mind with an expert at your side.
At RICHI, we go beyond project completion. With RICHI Servicee, we’re your dedicated partners in success. Count on us for expert guidance, minimal downtime, and optimized productivity. Choose RICHI for unmatched service and support.

Meet global product demands and quality standards with industry-leading pellet plant design, engineering, equipment, and construction services for pellet processors.

Your Partner Beyond Project Completion
2000+ cases
RICHI is the leading designer, manufacturer and builder of pellet plants in the world, completing over 2000 projects in 140 countries across 6 continents.
Read More
Increase plant productivity, profitability, and safety by integrating high quality equipment into your pellet production line. Over the years, RICHI has become China's top pellet equipment manufacturer. At the same time, RICHI has established valuable partnerships with the world's leading component and raw material manufacturers to bring you the best there is in technology, automation, and efficiency in pelleting plant machinery.

For nearly 30 years, RICHI has been providing best-in-class pellet plant equipment and services to clients across a variety of industries, sizes, and needs. We pride ourselves on the knowledge and skill that each team member possesses – from our technical sales team to our process design engineers. You can count on RICHI Machinery to take your operation to the next level of innovation, quality, and success.
Need help with your pellet manufacturing plant project? Contact us today.
ANIMAL FEED
BIOMASS
WOOD
ORGANIC FERTILIZER
AQUA FEED
CAT LITTER
MUNICIPAL WASTE RECYCLING
SPECIAL PELLET PRODUCTION
RICHI Machinery continues to deliver world class pellet mill equipment, pellet plant engineering and project solutions that add value to our customers in the animal feed, wood waste, agriculture waste, organic fertilizer, cat litter and special pellet products industries. Throughout the years, we RICHI Machinery have built strong brand, becoming industry-leading pellet machine manufacturer. We value integrity, promise quality, and prioritize your success.
Learn MoreWith our expert team, we precisely implement your process engineering requirements in pellet mill and pelletizing plant systems. No matter which industry you’re in – we understand your needs and deliver solutions that meet the highest standards.
At RICHI, quality comes first. Our pellet making machine and related pellet line equipment undergo rigorous quality controls to ensure they meet the highest standards. Rely on products that are durable, safe, and efficient.
With decades of experience in pellet machine and pellet production line production, we have earned a reputation as a trusted partner in various industries. Our expertise allows us to cover a wide range of applications.
Not only do we offer premium pelleting equipment, but we are also experts at designing, building, installing, and maintaining facilities from the ground up. Our expertise is within pellt plant process design, discovering the most efficient, productive, and profitable way to handle your materials in an end-to-end cycle.
○ RICHI MACHINERY
Keeping in touch with us is an effective way to solve all your problems. If you have any needs or questions, please leave your contact information, then RICHI technical consultants will send design, quotation, videos to your mailbox. You can also contact us directly via WhatsApp: +86 13838389622
Copyright©2015-2026 by HENAN RICHI MACHINERY CO., LTD. All rights reserved.