A central Chile fertilizer processor uses one FZLH420 pellet machine to produce 10 mm organic fertilizer pellets from stabilized manure and prepared agricultural residues.
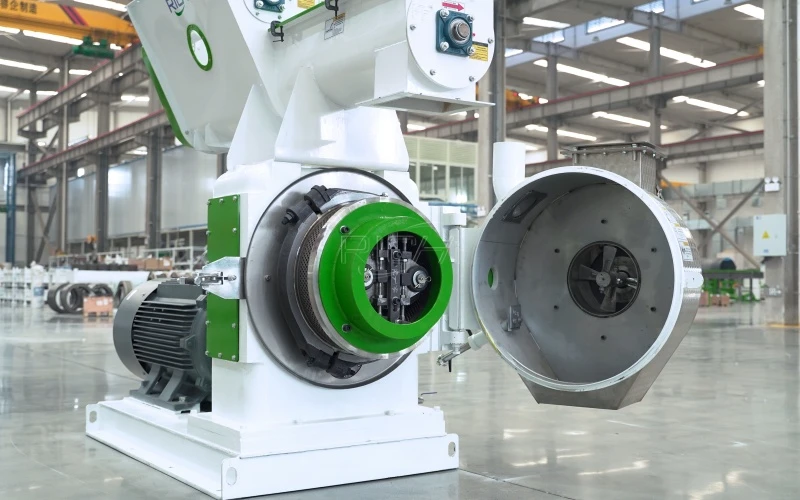
A medium-scale organic fertilizer manufacturer in central Chile added one FZLH420 Pellet Machine for Fertilizer in Chile to increase the capacity of its forming section. The plant aggregates livestock manure and suitable agricultural organic materials, then supplies pelletized fertilizer to distributors and farms serving vineyards, orchards, vegetable production and other commercial crops.
The customer already operated composting, crushing, mixing, moisture-control and storage equipment, so the project focused on one standalone ring-die pelletizer rather than another complete fertilizer line. The FZLH420 provides approximately 6–8 T/H of reference pelletizing capacity under suitable prepared-material conditions and produces a 10 mm cylindrical pellet as the main commercial specification.
Name:
Pellet Machine for Fertilizer
Country:
Chile
Date:
2026
Capacity:
6–8 T/H
Model:
FZLH420
Power:
90 kW
Raw materials:
Stabilized livestock-manure
Pellet Diameter:
10 mm
The factory's limiting stage was the conversion of prepared organic fertilizer into a compact, standardized product.
The customer did not need another manure-receiving area or a completely separate composting system. Mature fertilizer material was already being prepared in batches, but the forming section could not support the intended commercial volume efficiently.
One FZLH420 fertilizer granulator machine gives the plant a higher-capacity mechanical finishing route while allowing upstream biological treatment and formulation equipment to continue operating according to their own production rhythm.
This separation is important because composting is measured in days or weeks, while ring-die pelletizing processes prepared material much more quickly.
| Project Parameter | Configuration |
|---|---|
| Equipment | Organic fertilizer ring-die pellet machine |
| Model | FZLH420 |
| Quantity | 1 unit |
| Main Motor Power | 90 kW |
| Anti-Bridging Feeder Power | 3 kW |
| Forced Feeder Power | 1.5 kW |
| Ring Die Inner Diameter | 420 mm |
| Available Pellet Diameter | 4–12 mm |
| Main Project Pellet Diameter | 10 mm |
| Reference Capacity | Approximately 6–8 T/H under suitable prepared-material conditions |
| Main Feedstock | Stabilized livestock-manure fertilizer mixtures |
| Secondary Organic Material | Prepared corn residues and other qualified agricultural organic matter |
| Installation Type | Standalone pelletizing upgrade in an operating fertilizer factory |
The 6–8 T/H value refers to the pelletizing section. It does not describe fresh-manure intake, composting capacity or guaranteed finished-fertilizer output for every formulation.
A 90 kW fertilizer pelletizer would be excessive for a small farm processing only its own manure occasionally.
This customer operates differently. It collects organic materials from multiple agricultural and livestock businesses and processes mature fertilizer material in commercial batches.
Prepared compost can accumulate ahead of the pelletizing section. The FZLH420 can then operate for concentrated production periods rather than needing to run continuously throughout every day of the year.
This campaign-based arrangement makes 6–8 T/H practical while keeping the project below the larger FZLH520 class, which would require substantially more prepared material and supporting capacity.
The fertilizer plant serves an agricultural market where vineyards, fruit production, vegetables and livestock activities operate within the same broader central-zone economy.
This gives the customer access to both fertilizer demand and several types of organic feedstock.
Pig manure is collected through commercial livestock operations, while cattle manure can enter from dairy or beef farms within the wider procurement area.
Crop residues are evaluated seasonally rather than assumed to be available at the same quantity throughout the year.
The customer therefore builds its raw-material plan around contracted tonnes and actual fertilizer sales rather than theoretical regional waste volumes.
Fresh pig manure is biologically active and commonly contains too much water for direct ring-die pelletizing.
Drying alone does not solve that problem.
The material first passes through an appropriate stabilization or composting process so that active decomposition is substantially reduced and the manure becomes suitable for fertilizer formulation.
Moisture, aeration and carbonaceous material are managed during this stage according to the condition of the incoming manure.
Only mature material proceeds to the mechanical fertilizer section.
Cattle manure differs according to housing and collection method.
Material scraped from a yard can contain more soil and mineral contamination, while manure mixed with straw bedding may contain substantially more fibre.
Both conditions affect pelletizing.
Soil and sand increase ash and wear. Long bedding fibres can interfere with feeding and ring-die compression unless they are adequately decomposed or reduced in size.
The factory therefore evaluates cattle manure by condition rather than treating every delivery as one uniform material.
Maize production creates stalks, leaves and other dry crop residues that can contribute carbon and physical structure during compost preparation.
The customer does not add a fixed 20% corn-stalk fraction simply to make fertilizer pellets harder.
Fresh or dry stalk material is chopped before composting. During biological treatment, the plant fibre begins to break down and becomes more compatible with the manure fraction.
If long fibres remain after maturation, the material receives additional size reduction before mixing and pelletizing.
The useful amount depends on manure moisture, carbon-to-nitrogen balance, maturity and the specification of the final fertilizer.
Organic feedstocks vary too much for one fixed manure-and-stalk formula to remain appropriate throughout the year.
Pig manure from one supplier can differ from another in moisture, nutrient concentration and ash. The same applies to cattle manure and crop residues.
Commercial formulation therefore considers:
The FZLH420 converts the prepared formulation into a physical pellet. It does not balance nutrient ratios inside the machine.
Growers of grapes, fruit and vegetables can use organic fertilizer, but these crops do not automatically require the same nutrient concentration or application rate.
Vineyard soil, irrigation water, crop stage, expected yield and existing nutrient status all influence fertilizer management.
The factory therefore does not market one manure pellet as an identical agronomic product for every vineyard, orchard and vegetable farm.
Its role is to manufacture fertilizer to a documented product specification that distributors and growers can then use within an appropriate fertilization program.
Commercial manure-based fertilizer needs more than a visually uniform pellet.
The customer checks representative fertilizer batches for nutrient and physical parameters relevant to the intended product.
Salt loading deserves particular attention because manure-based materials can contain substantial soluble minerals depending on animal diet and manure management.
A mechanically strong pellet with an unsuitable nutrient or salt profile would still be the wrong fertilizer for a sensitive crop or soil.
Laboratory analysis therefore remains upstream of commercial product claims.
The Pellet Machine for Fertilizer in Chile operates near the end of the manufacturing route, after biological treatment and formulation.
A practical process for this factory follows these stages:
Each stage solves a different process requirement. Ring-die compression cannot substitute for composting, formulation, drying or finished-product cooling.
Composted manure can form hardened lumps during maturation and storage.
These lumps are not suitable for accurate mixing or stable ring-die feeding.
The customer therefore reduces compacted material before formulation.
Crushing also helps create a more consistent particle distribution between fine manure compost and fibrous plant components.
The objective is not to turn the fertilizer into ultrafine dust. It is to eliminate oversized material that would disrupt mixing or pellet formation.
Prepared corn residue and bedding fibre can remain visible even after composting.
Long strands are undesirable at the FZLH420 inlet because they can bridge inside hoppers and create irregular loading at the forced feeder.
For many manure-based ring-die fertilizer mixtures, preparing the majority of the material to a few millimeters provides a practical basis for stable pelletizing.
Approximately 2–5 mm can be used as a useful engineering reference for many prepared materials, with the final setting determined from actual fibre condition and pelletizing trials.
Grinding finer than necessary adds electricity consumption and dust without automatically improving fertilizer quality.
Compost maturity and pelletizing moisture are separate process questions.
A material can be biologically mature and still contain more water than the ring-die section can handle efficiently.
The factory therefore measures moisture after stabilization and mechanical preparation.
If the mixture is too wet, feeding can become unstable and pellets may remain soft. If the material is excessively dry, fines and compression resistance can increase.
The operator establishes the working condition from feeder behavior, motor load, ring-die performance and finished-pellet condition rather than using exactly 18% for every formula.
The factory has thermal moisture-control equipment, but not every batch needs the same drying duty.
Material that has already lost sufficient moisture through composting and covered maturation may require little thermal treatment.
Wetter batches can require additional drying before the FZLH420.
This approach avoids paying for unnecessary water evaporation while still protecting the pelletizing section from material that is too wet.
The machine should receive suitably conditioned fertilizer rather than being expected to overcome excessive moisture through motor power.
The Chilean customer uses a 10 mm ring die for its principal fertilizer pellet.
This size falls within the FZLH420's 4–12 mm operating range and creates a robust cylindrical product for bulk handling, bagging and field distribution.
If the market later requires a smaller fertilizer pellet, another compatible ring die can be evaluated.
The customer does not claim that 10 mm fertilizer contains more nutrients than a 6 mm product made from the same formulation.
Pellet diameter determines physical form, not nutrient concentration.
It would also be inaccurate to describe a 10 mm manure pellet as automatically providing a specific controlled-release performance.
Breakdown after field application depends on fertilizer composition, pellet density, moisture, microbial activity, irrigation, rainfall, soil conditions and application method.
Changing pellet diameter can influence exposed surface area and physical breakdown, but it is only one part of the complete fertilizer behavior.
Any nutrient-release claim therefore has to come from product testing rather than from ring-die diameter alone.
Mature compost mixtures do not always discharge from a hopper as freely as mineral granules.
Fine manure material can compact, while residual plant fibre can create arches above the outlet.
The FZLH420 uses a 3 kW anti-bridging feeder to keep material moving toward the pelletizing section.
The 1.5 kW forced feeder then delivers the prepared material into the ring-die chamber at a controlled rate.
These components improve feeding stability but do not make long stalks, wet manure or large compost lumps acceptable feed.
Sudden surges of low-density organic material can create rapid changes in motor load.
The operator therefore regulates feed rate instead of loading the hopper as aggressively as possible.
Motor current, throughput and pellet appearance are monitored together during production.
If current rises while throughput falls, operators can investigate moisture, feed consistency, die condition, fibre length or excessive feeder rate.
Additional motor power is not a substitute for stable material preparation.
This distinction is essential when sizing the project.
A 6–8 T/H FZLH420 does not mean the factory receives only 6–8 tonnes of fresh manure for every hour of pellet production.
Fresh manure contains substantial water. Composting also causes mass loss through moisture removal and biological decomposition.
Screening removes contaminants, and formulation can introduce other fertilizer components.
The amount of raw manure required to support 6–8 T/H of prepared pellet feed therefore has to be calculated from actual moisture and mass balance.
The factory does not need to make 6–8 tonnes of mature compost every hour continuously.
Compost can accumulate in a covered mature-material storage area before a granulation campaign begins.
The pelletizer can then process that inventory over a shorter period.
This allows a medium fertilizer business to use a multi-ton-per-hour ring-die machine without pretending that every biological and mechanical stage has exactly the same hourly flow.
A dense manure-rich fertilizer can behave differently from a lighter mixture containing more crop fibre.
Actual FZLH420 output depends on:
The customer therefore uses 6–8 T/H as a reference operating range rather than promising that every fertilizer formula will remain at exactly 8 T/H.
Fresh fertilizer pellets leave ring-die compression warmer than the surrounding environment.
Cooling allows the pellet to stabilize before screening and packaging.
This step should not be confused with large-scale moisture removal.
If prepared fertilizer enters the FZLH420 with excessive water, the cooler cannot economically perform the work of a dryer.
Upstream moisture control remains the correct place to solve that problem.
After cooling, qualified pellets are separated from fines and broken material.
A rising fines level can indicate moisture imbalance, excessive residual fibre, unsuitable die conditions, wear or rough mechanical handling.
The operator therefore treats screening data as a useful indicator of process stability.
Recovered fines can be returned through a controlled route where the product specification and plant design allow it.
Ring-die compression increases bulk density compared with loose compost, but finished pellet density varies with the fertilizer mixture.
Fine mature manure behaves differently from a high-fibre crop-residue blend.
Moisture, ash and die characteristics also affect the physical result.
The factory therefore evaluates the actual product rather than advertising one density value for every manure formula.
The FZLH420 changes handling form and bulk characteristics.
It does not create nitrogen, phosphorus or potassium.
If the incoming formula contains insufficient nutrients, mechanical compression cannot improve the analysis.
The same principle applies when excessive low-nutrient crop residue is included: the ring die can form a strong pellet while the fertilizer remains nutritionally dilute.
Fertilizer formulation therefore has to be complete before the product reaches the machine.
Raw manure can create odor, microbial activity and storage problems.
The pellet machine should not receive credit for solving those issues by itself.
Proper composting and maturation are responsible for stabilizing the organic material before mechanical finishing.
Pelletizing then improves densification, packaging and transport characteristics of the mature fertilizer.
Keeping these functions separate results in a more realistic process design.
Manure collected from open yards can contain soil and small stones.
Corn residues gathered close to the ground can introduce additional mineral contamination.
These materials increase ash without providing useful organic fertilizer value and can accelerate die and roller wear.
Receiving inspection, screening and sensible raw-material handling are therefore part of maintenance control.
Cleaner material can often improve wear performance more effectively than simply specifying harder components.
Wire, bolts and broken farm hardware can enter manure and crop-residue streams during collection.
Appropriate magnetic protection ahead of fine processing helps reduce the risk of ferrous metal reaching the pelletizing system.
Magnets do not remove stones, plastic or non-ferrous objects, so visual inspection and screening remain necessary.
The FZLH420 organic fertilizer pellet machine can only use its reference capacity when the mixing section keeps the feeder supplied.
A batch mixer operating at a much lower average rate can become the actual plant limitation.
The customer therefore evaluates mixer batch weight, cycle time and transfer capacity together with the pelletizer.
A suitable intermediate buffer can separate batch mixing from continuous pellet feeding.
This keeps the FZLH420 from stopping every time another fertilizer batch is being prepared.
The FZLH420 uses a 90 kW main motor together with the 3 kW anti-bridging feeder and 1.5 kW forced feeder.
The complete section can also include conveyors, crusher, mixer, cooler, screen, dust collection and moisture-control equipment.
The factory therefore checks transformer capacity, motor starting, protection, cable sizing and simultaneous electrical demand before installation.
Connected power should be calculated from the complete operating section rather than the pelletizer nameplate alone.
The machine location has to support both production and service work.
Installation planning includes inlet height, discharge elevation, structural support, electrical routing and access around the ring-die and roller area.
A position that physically accommodates the machine but leaves insufficient room for die inspection or component removal creates avoidable maintenance difficulty.
This is particularly important in a retrofit where the surrounding mixer, conveyors and storage equipment are already fixed in place.
The FZLH420 is prepared for sea transport from Qingdao to San Antonio before inland delivery to the central Chile facility.
This route is practical for machinery entering Chile's central macrozone and continuing by road to agricultural regions such as O'Higgins or Maule.
Before shipment, the customer can prepare the foundation, electrical connection and equipment interfaces using confirmed installation data.
Ocean schedules, terminal handling and inland transport are coordinated according to the actual cargo arrangement rather than one fixed delivery period.
If fertilizer sales grow, the factory should first determine which section is restricting output.
The pelletizer may still have reserve capacity while compost maturation, crushing, mixing, drying, cooling or bagging reaches its limit.
In that situation, adding another pellet machine would create more installed capacity without increasing saleable fertilizer.
Expansion decisions are therefore based on measured material flow through each process stage.
If mature fertilizer regularly accumulates ahead of the first machine and downstream equipment can support more output, a second FZLH420 can be evaluated.
Two identical units would provide approximately 12–16 T/H of combined reference capacity for the pelletizing section.
This does not mean the whole factory immediately becomes a 16 T/H fertilizer plant.
Composting, formulation, mixer capacity, moisture control, cooling, screening, packing and electrical infrastructure would all need sufficient capacity before the additional pelletizer could be fully utilized.
The FZLH420 supports fertilizer pellets within the 4–12 mm range.
If distributors later request a 6 mm or 8 mm product, the customer can evaluate another ring-die specification rather than installing a completely different granulation technology.
The plant would still need to confirm how the smaller diameter affects throughput, compression resistance and the downstream product specification.
Offering several sizes is useful only when there is a real market reason to maintain them.
A Pellet Machine for Fertilizer in Chile should be selected from the amount of mature, prepared fertilizer available for mechanical forming rather than from the fresh tonnes of manure generated by nearby farms. Manure condition, compost maturity, crop-residue content, particle size, moisture and required pellet diameter all affect usable machine capacity.
For another Chilean organic fertilizer production project, RICHI Machinery would first review manure types, annual collection volume, composting method, mature-material output, moisture after maturation, crop-residue condition, fertilizer analysis, mixer capacity, target pellet size, drying requirement, cooling and screening capacity, operating hours, electrical supply and intended agricultural market.
Those details determine whether one FZLH420 provides the right scale or whether another FZLH model would better match the customer's actual fertilizer production system.
Having the right mix of reliable, high-quality pellet machine and pelletizing systems and expert support is essential to your success. Watch how our end-to-end feed pellet plant solutions have helped our customers optimize their performance.
Our customized and future-proofed turnkey pellet plant solutions is designed with you at the core. From vision to reality and beyond, our team stays connected with yours. Giving you peace-of-mind with an expert at your side.
At RICHI, we go beyond project completion. With RICHI Servicee, we’re your dedicated partners in success. Count on us for expert guidance, minimal downtime, and optimized productivity. Choose RICHI for unmatched service and support.

Meet global product demands and quality standards with industry-leading pellet plant design, engineering, equipment, and construction services for pellet processors.

Your Partner Beyond Project Completion
2000+ cases
RICHI is the leading designer, manufacturer and builder of pellet plants in the world, completing over 2000 projects in 140 countries across 6 continents.
Read More
Increase plant productivity, profitability, and safety by integrating high quality equipment into your pellet production line. Over the years, RICHI has become China's top pellet equipment manufacturer. At the same time, RICHI has established valuable partnerships with the world's leading component and raw material manufacturers to bring you the best there is in technology, automation, and efficiency in pelleting plant machinery.

For nearly 30 years, RICHI has been providing best-in-class pellet plant equipment and services to clients across a variety of industries, sizes, and needs. We pride ourselves on the knowledge and skill that each team member possesses – from our technical sales team to our process design engineers. You can count on RICHI Machinery to take your operation to the next level of innovation, quality, and success.
Need help with your pellet manufacturing plant project? Contact us today.
ANIMAL FEED
BIOMASS
WOOD
ORGANIC FERTILIZER
AQUA FEED
CAT LITTER
MUNICIPAL WASTE RECYCLING
SPECIAL PELLET PRODUCTION
RICHI Machinery continues to deliver world class pellet mill equipment, pellet plant engineering and project solutions that add value to our customers in the animal feed, wood waste, agriculture waste, organic fertilizer, cat litter and special pellet products industries. Throughout the years, we RICHI Machinery have built strong brand, becoming industry-leading pellet machine manufacturer. We value integrity, promise quality, and prioritize your success.
Learn MoreWith our expert team, we precisely implement your process engineering requirements in pellet mill and pelletizing plant systems. No matter which industry you’re in – we understand your needs and deliver solutions that meet the highest standards.
At RICHI, quality comes first. Our pellet making machine and related pellet line equipment undergo rigorous quality controls to ensure they meet the highest standards. Rely on products that are durable, safe, and efficient.
With decades of experience in pellet machine and pellet production line production, we have earned a reputation as a trusted partner in various industries. Our expertise allows us to cover a wide range of applications.
Not only do we offer premium pelleting equipment, but we are also experts at designing, building, installing, and maintaining facilities from the ground up. Our expertise is within pellt plant process design, discovering the most efficient, productive, and profitable way to handle your materials in an end-to-end cycle.
○ RICHI MACHINERY
Keeping in touch with us is an effective way to solve all your problems. If you have any needs or questions, please leave your contact information, then RICHI technical consultants will send design, quotation, videos to your mailbox. You can also contact us directly via WhatsApp: +86 13838389622
Copyright©2015-2026 by HENAN RICHI MACHINERY CO., LTD. All rights reserved.